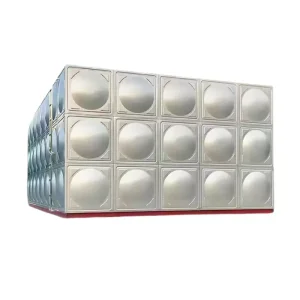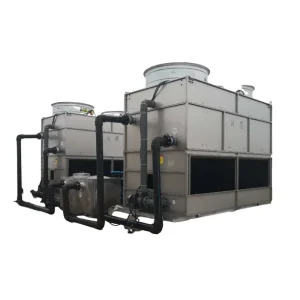
Engineered thermal exchange units, heavy-duty ventilation systems, and subterranean storage tanks certified to demanding global industrial standards.

Years Engineering Experience
Fabrication Base (Dezhou, CN)
Global EPC Cooperative Clients
CE Factory-Tested Compliance
Urban density, severe climate events, and strict sustainable water policies are redefining the procurement specifications of subterranean retention and attenuation assets.
Commercial land costs in hyper-dense metropolitan areas make surface detention ponds unviable. Industrial buried stormwater tanks maximize above-ground footprint for logistics yards, car parking, or manufacturing infrastructure while retaining vast hydrological volumes below grade.
Multinational EPC contractors are mandated to integrate Sustainable Drainage Systems (SuDS) and Low Impact Development (LID) standards. Engineered tanks control peak runoff rates, intercept particulate matter, and harvest rainwater for industrial greywater reuse cycles.
Leading enterprises minimize municipal capital expenditure by procuring dual-purpose buried infrastructure that handles both stormwater buffering and NFPA 22/EN 12845 fire-fighting water reserves via compartmentalized baffle partitions.
From hydrostatic uplift resistance to continuous cathodic protection, our factory in Dezhou leverages advanced metal forming and precision welding technologies.
| Structural Parameter | SUS304 / SUS316 Stainless Matrix | High-Temp Sintered Enamel Steel | Reinforced Buried Modular Composites |
|---|---|---|---|
| Primary Application | Potable storage, sanitary buffer & critical fire reserve | Municipal storm collection & high-volume wastewater | Heavy vehicular traffic attenuation & underground soakaway |
| Corrosion Resistance | Passive chromium-oxide layer; SUS316 Mo added for chlorides | Glass-fused-to-steel inert barrier (pH 2–11 resistance) | Galvanized external armor + internal polymeric protection |
| Structural Load Capability | Engineered internal tie-rods; designed for basement plant rooms | High tensile strength; supports deep hydrostatic pressure | SLW 60 (60-ton truck load) certified with minimal soil cover |
| CE Directives & Testing | EN 1090-2 (Execution of steel structures), Factory ISO 9001 | EN ISO 28765, EN 10025 structural conformity | EN 12845 (Automatic fire sprinkler systems water reservoirs) |
Operating in Shandong's premier manufacturing corridor provides seamless access to heavy hot-dip galvanized steel, certified stainless coils, and specialized tooling. This cluster efficiency reduces lead times by 35% compared to non-specialized regions.
Every underground tank panel undergoes automatic longitudinal submerged arc welding or robotic plasma cutting, followed by 100% dye penetrant and ultrasonic non-destructive examination (NDE) prior to containerization.
Procuring directly from our 12,000 m² facility removes domestic brokers and overseas trading agents. EPC contractors receive full material test certificates (MTRs 3.1) and engineering drawings straight from the manufacturer.
Smart sensors, anti-buoyancy computational modeling, and integrated environmental control form the future of below-ground stormwater containment.
Integration of CE-marked hydrostatic level transmitters and turbidity monitors connected via Modbus/BACnet to building automation frameworks for predictive stormwater discharge.
Finite element modeling of high water table kinetics. Standardized concrete deadman strap connections safeguard against tank flotation during extreme flood events.
Coupling buried retention water with industrial closed circuit cooling towers as emergency heat sink reserves, improving enterprise energy efficiency and emergency operational stability.
Complete skidded pump stations pre-piped inside access manholes, reducing site civil construction timelines and eliminating field pipe-fit errors.
Exporting heavy engineered equipment requires rigorous adherence to multinational building directives, logistics optimization, and third-party validation.
Every stormwater tank system exported to the European Economic Area carries full compliance dossiers conforming to EN 1090-1 execution classes, backed by factory production control (FPC) certificates and CE markings.
Panels and components are secured on custom steel cradles with vapor-corrosion-inhibitor (VCI) protective wrapping, designed specifically for harsh maritime shipping via Qingdao and Tianjin ports.
Our bilingual structural and fluid dynamics engineers provide remote installation supervisory services, detailed 3D step-by-step assembly models, and rapid spare-parts availability worldwide.
Essential guidance for EPC contractors, consulting engineers, and procurement specialists evaluating buried stormwater and fire water solutions.
Depending on the soil chemistry and chosen grade (SUS304, SUS316, or sintered enamel), our buried tank systems are engineered for a design working life of 30 to 50+ years, featuring internal cathodic protection and heavy external anti-corrosion barrier coatings.
Every modular panel features precision CNC-punched bolt holes and specialized EPDM/silicone food-grade gasket cords, or high-penetration robotic TIG welding. Tanks are hydrostatically leak tested before project hand-off and comply with strict zero-loss criteria.
Yes. Our reinforced buried water tanks are engineered with heavy top-slab load-bearing struts rated for SLW 30 to SLW 60 live vehicle axle loadings, allowing seamless installation under heavy logistics yards and access roadways.
Absolutely. We routinely collaborate with world-leading third-party inspection agencies including SGS, Bureau Veritas (BV), and TÜV to witness hydrostatic pressure tests, weld ultrasonic tests, and raw material mill certifications prior to departure from China.
Explore our certified solutions engineered for global industrial infrastructure, commercial complexes, and municipal engineering projects.