Explore our factory-built geothermal condensing apparatus, heavy-duty cooling towers, specialized ventilation fans, and industrial reserve tanks built in Dezhou, China.

The international push for decarbonization and geothermal utilization requires cooling towers designed to operate under unconventional enthalpy parameters, brine chemistry, and non-condensable gas emissions.
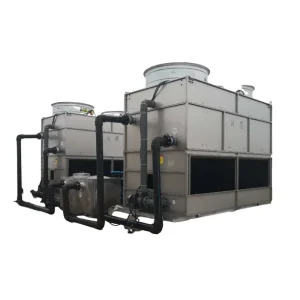
Modern geothermal power relies on Organic Rankine Cycles (ORC) where hydrocarbon or refrigerant working fluids require precise cold condensing. Closed-circuit cooling towers with high-efficiency alloy coils ensure process isolation, avoiding fluid contamination while providing exceptional enthalpy drop.
Geothermal steam and condensate carry elevated levels of hydrogen sulfide (H₂S), ammonia, chlorides, and silica. Traditional cooling materials degrade rapidly. Our specialized geothermal models integrate fiberglass reinforced polyester (FRP), vinyl ester matrices, and titanium or SUS316L coil bundles to withstand corrosive chemical assault.
Ground-source heat pump (GSHP) systems require balancing cooling towers for high-load summer rejection to prevent ground thermal saturation. Our variable-frequency driven (VFD) axial fan cooling units dynamically equalize underground thermal reservoirs, maintaining balanced sub-surface COP year-round.
Comparing engineering priorities across EPC contractors, energy conglomerates, and industrial plant managers when sourcing geothermal heat ejection systems.
| Procurement Pillar | Geothermal Plant Requirement | Standard Open Tower Limitation | Fengdun Engineering Solution |
|---|---|---|---|
| Corrosion Resistance | Exposure to 250+ ppm H₂S, ammonia, high TDS brine | Standard galvanized sheets fail within 24–36 months | Pultruded FRP structural frames, vinyl-ester resin coating, 316L/Titanium tubing |
| Thermal Parasitic Load | Minimizing internal electricity consumption per MW heat rejected | Fixed speed belt-driven fans with high aerodynamic resistance | Direct-drive aerofoil mixed flow impellers paired with IE4 permanent magnet VFD motors |
| Fouling & Scaling Control | Silica precipitation and mineral scaling at elevated ΔT | Cellular film fills clog rapidly requiring chemical acid cleaning | Clog-resistant splash bar grid fills with non-clogging target nozzles for easy hydro-jetting |
| Drift Loss & Environmental | Strict municipal limits on hazardous steam dispersion | Drift rate > 0.02% of circulating water volume | High-efficiency cellular drift eliminators achieving <0.0005% drift volume loss |
| Structural Integrity | Zone 4 seismic resilience, 150+ km/h typhoon wind loads | Modular lightweight residential-grade assembly | Heavy-gauge gusset-reinforced internal framework tested to GB/T & EN standards |
From municipal district heating auxiliary cooling to heavy petrochemical process loops, Fengdun delivers engineered architectures customized to plant layout.
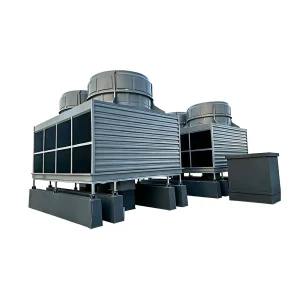
Complete counterflow cooling systems engineered for flash steam geothermal power stations. Optimized for high volume water recirculation with integrated non-condensable gas (NCG) extraction fan ducting and corrosion-proof hot-water basins.
Direct geothermal brine mining (Lithium, Boron, Silica recovery) demands rigorous process loop temperature control. Our closed-loop cooling towers prevent salt crystallization inside critical heat exchangers via managed dry/wet multi-stage control.
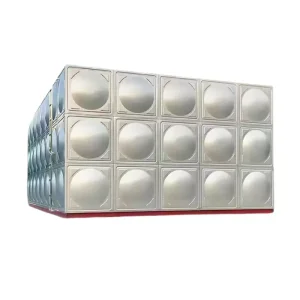
For applications where cooling tower return water must directly interface with low-pressure barometric condensers. Our systems balance hydraulic head loss, entrained gas degassing, and microbiological control through engineered water storage tanks.
Reliability starts at our 12,000 m² manufacturing plant in Dezhou, Shandong. We provide comprehensive export documentation, third-party inspection, and certified compliance.
As an original equipment manufacturer (OEM/ODM), every structural component, fan shroud, water tank, and damper is made in our plant. Overseas buyers bypass brokerage fees, gain live factory audit access, and directly communicate with design engineers.
Products are engineered to conform to American CTI (Cooling Technology Institute) Standard 201, European CE directives, ASHRAE 90.1 energy performance standards, and ISO 9001:2015 quality management benchmarks.
Full pre-shipment quality verification protocols by Bureau Veritas (BV), SGS, or TÜV Rheinland can be integrated into your letter of credit (LC) terms, including ultrasonic weld testing and hydrostatic vessel verification.
Pioneering sustainable cooling tower operations with lower water footprint and predictive machine-learning monitoring.
Deploying hybrid wet/dry cooling architectures that utilize dry sensible cooling during lower ambient temperatures, reducing geothermal plant water consumption by up to 45% annually.
Integrating wireless vibration sensors on fan drive shafts, laser alignment trackers, and real-time fill packing pressure differential sensors to dynamically flag mineral accumulation before thermal performance drops.
Applying fluoropolymer-infused nano-composite protective barriers to heat exchanger coil surfaces, resisting silica scale adhesion and eliminating the necessity for hazardous chemical acid flushing.
Essential technical, manufacturing, and operational insights for procurement directors and facility engineers.
Geothermal cooling towers manage significantly higher continuous heat rejection rates, lower cold-water approach temperatures, and fluids carrying corrosive non-condensable gases (NCG), hydrogen sulfide, and dissolved solids. They require specialized FRP or stainless structural materials, non-clogging distribution nozzles, and heavy-duty industrial fan designs.
Open counterflow cooling towers offer lower initial capital expenditure and suit high-flow, lower-fouling applications. Closed-circuit cooling towers isolate the process fluid inside sealed heat exchange coils, ensuring zero contact with atmospheric dust or pollutants, making them mandatory for high-precision Organic Rankine Cycle (ORC) condensers and induction equipment.
We configure equipment with heavy vinyl ester resin FRP casings, 316L stainless steel structural hardware, silicon-carbide or titanium tubing for heat exchange bundles, and anti-corrosive epoxy-polyurethane coatings for any structural carbon steel components.
Every export order is accompanied by detailed structural engineering calculation books, mill test certificates (MTC 3.1), CE declarations of conformity, ISO certificates, factory hydrostatic test reports, packing slips, dynamic balance reports, and Certificates of Origin.
Please provide the circulating water flow rate (m³/h), hot water inlet temperature, cold water outlet temperature, design ambient wet-bulb temperature, water chemistry analysis (TDS, pH, chlorides), available footprint, and electrical power specifications (voltage, frequency, phase).
Yes. We specialize in custom OEM/ODM fabrication. Because our 12,000 m² factory controls laser cutting, sheet metal bending, and welding in-house, towers and sectional water tanks can be dimensionally configured to fit existing plant footprints or rooftop layouts.
Review our heavy ventilation, duct management, and water containment products built for extreme duty cycles.