Explore precision-fabricated cooling towers, specialized industrial water storage tanks, and heavy-duty smoke extract fans manufactured in Dezhou's national HVAC manufacturing hub.
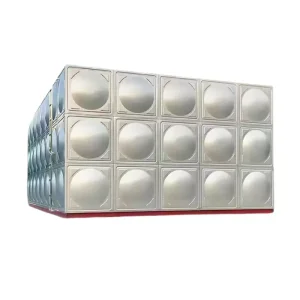
Heavy-duty SUS304 and SUS316 sanitary welded storage modules with food-grade internal passivation and certified leak-proof modular framing.
View Specifications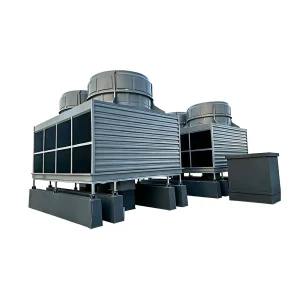
Aerodynamically optimized counterflow square design featuring high-efficiency PVC film fill packing and corrosion-proof FRP or galvanized housings.
View Specifications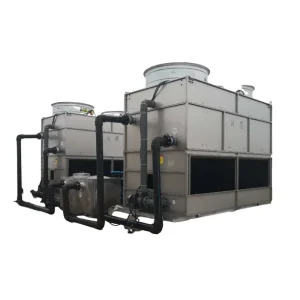
Completely enclosed coil loop preventing scale build-up, biological contamination, and particulate fouling in sensitive induction or chemical systems.
View Specifications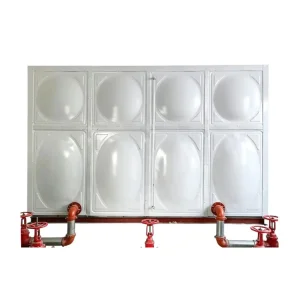
Engineered high-temperature sintered enamel panels offering non-toxic inert surfaces, outstanding chemical barrier strength, and high tensile structural integrity.
View Specifications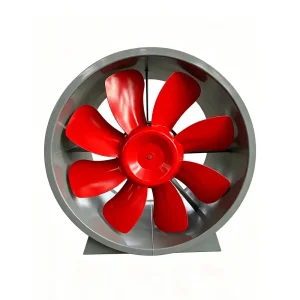
High-temperature rated emergency evacuation axial fans delivering high cubic meter displacement during industrial fire mitigation protocols.
View Specifications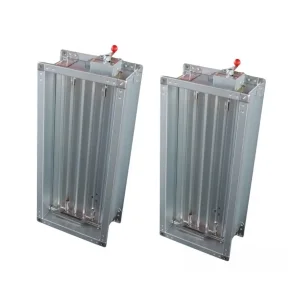
Heavy-gauge galvanized steel safety dampers featuring certified 70°C and 280°C fusible safety links for immediate duct smoke partition sealing.
View Specifications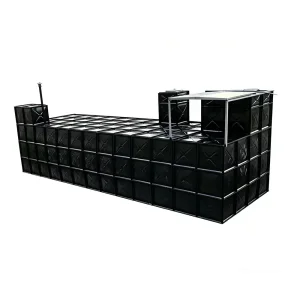
Underground anti-hydrostatic pressure structural water chambers developed to optimize surface spatial efficiency while securing municipal fire reserves.
View Specifications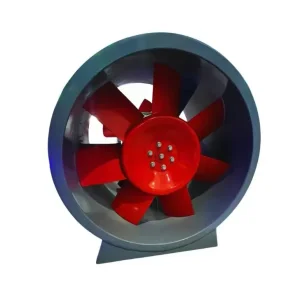
Dual-purpose continuous comfort ventilation and 280°C/2h emergency smoke clearance fans engineered with dynamic balance precision.
View SpecificationsIn modern process industries, industrial refrigeration, and large-scale power production, the requirement for dependable heat rejection equipment has shifted from basic thermal dissipation to stringent life-cycle energy stewardship. An OEM Imeco Cooling Tower and associated evaporative condenser systems embody decades of design innovation characterized by optimized coil geometries, minimized approach temperatures, and robust counterflow airflow dynamics.
Global industrial operators, cold storage logistics hubs, chemical processing plants, and food packaging giants require replacement components, complete retrofit assemblies, and drop-in replacements that adhere faithfully to OEM Imeco specifications. Modern engineering demands that replacement and OEM-grade towers eliminate thermal degradation over decades of continuous operation while coping with fluctuating ambient wet-bulb conditions.
Every cooling system fabricated in our facility undergoes rigorous verification against CTI (Cooling Technology Institute) STD-201 and international thermodynamic balance standards.
International EPC contractors, central utility managers, and cold storage procurement directors seek exact thermodynamic matches, low sound profiles, and proven corrosion barriers when evaluating heat rejection suppliers.
Direct manufacturer pricing from Shandong Fengdun eliminates multiple middle-tier distributors, delivering factory-direct cost efficiency while maintaining strict adherence to high-spec metallurgy including hot-dip galvanized steel frames and SUS304/SUS316 heat exchange coils.
Retrofit operations cannot afford structural roof modification or piping alterations. Our custom OEM engineering matches exact Imeco basin configurations, pipe centerlines, and structural beam anchor locations, cutting plant downtime to minimum scheduled shutdowns.
Full mill test certificates (MTR) for all steels, weld inspection mapping, third-party hydro-testing reports by SGS/BV/TÜV, and CE/ISO 9001 quality audit trails provide immediate clearance for industrial insurance and municipal safety regulatory compliance.
Comparing heat rejection principles across process cooling, ammonia industrial refrigeration, and critical facilities to determine optimal hardware selection.
| Architecture Typology | Thermodynamic Process | Fouling Risk Factor | Target Industrial Application | Primary Material Matrix |
|---|---|---|---|---|
| Closed-Circuit OEM Tower | Indirect evaporative heat transfer via sealed serpentine coils | Near Zero (Internal loop isolated) | Induction melting, data centers, clean petrochemical loops | SUS304 / 316 Stainless or HDG elliptical tube bundles |
| Open Counterflow Tower | Direct liquid-to-air counter-current interface over PVC packing | Moderate (Atmospheric airborne contact) | Central district HVAC chillers, plastics molding, metal stamping | FRP casing, structural HDG steel, virgin PVC / PP fill |
| Evaporative Imeco-Style Condenser | Direct refrigerant phase change (vapor to liquid) within pressurized coils | Low (Continuous spray wash with biocide) | Ammonia (R717) cold chain, CO2 subcritical cascade, brewery systems | Seamless carbon steel tubes, hot-dip galvanized post-fabrication |
| Hybrid Adiabatic Cooler | Sensible dry cooling assisted by micro-spray during wet-bulb peaks | Negligible (Dry operation > 80% annual hours) | Water-scarce arid regions, remote mining extraction, microturbines | Hydrophilic aluminum fins, copper/stainless inner circuits |
Incorporates high-efficiency, wide-chord extruded aluminum or FRP airfoil fan blades dynamically balanced to ISO 1940 G2.5. Direct-drive permanent magnet synchronous motors (PMSM) or rugged gearboxes provide continuous variable-frequency flow control with reduced acoustic emission.
Engineered non-clogging large-orifice target nozzles fitted to balanced PVC/PP header manifolds ensure uniform hydraulic spray coverage over all coil tubes and fill channels, preventing dry spots that trigger rapid calcium and silicate scaling.
Tri-pass wave eliminators engineered from UV-stabilized PVC limit droplet carryover to less than 0.001% of circulating water volume, completely eliminating Legionella transmission risks and preserving chemical treatment reserves.
Our 12,000 m² factory in Dezhou leverages complete upstream supply lines, precision laser cutting, automatic robotic tube bending, and rigorous factory acceptance testing before export dispatch.
All OEM closed-circuit coils and evaporative condenser circuits are manufactured according to ASME Boiler and Pressure Vessel Code Section VIII and European Pressure Equipment Directive (PED 2014/68/EU).
Completed coil assemblies undergo structural acid pickling and immersion in a 450°C molten zinc bath (yielding ≥ 610 g/m² coating weight), sealing every weld point against severe salt-spray and acidic atmospheres.
Coils are pneumatically tested under water at 2.5 MPa for 30 consecutive minutes followed by helium mass spectrometer sniff testing to confirm total hermetic safety before cabinet casing assembly.
Engineered with standardized transport dimensions compatible with 40ft Open Top (OT) and High Cube (HC) sea containers, equipped with certified heavy crane rigging lugs for fast port-to-site offloading.
Integrating smart sensory feedback loops, AI-managed psychrometric fan staging, and advanced metallurgy to meet net-zero industrial sustainability mandates.
Built-in vibration transmitters on fan motor shafts, differential pressure monitors across eliminator packs, and ultrasonic sump depth gauges deliver continuous telemetry via Modbus/BACnet protocols to factory DCS control suites.
Secondary dry finned sensible desuperheater coils installed above the evaporative spray zone raise the exhaust air temperature, shifting leaving air psychrometrics to completely eliminate visible winter plume fog in urban locations.
Pioneering water-shedding nano-ceramic and graphene barriers applied to exterior sheet metal and fin stock offering 3,500+ hours of ASTM B117 salt fog endurance for extreme maritime off-shore installations.
Maintain plant thermodynamic and safety continuity with our certified soundproof cabinet fans, mixed-flow inline exhausters, and industrial water storage tanks.
Precision indirect coil cooling unit engineered for clean process fluids, metallurgical furnaces, and zero-contamination applications.
Request Technical Data
Vitreous sintered enamel coated structural steel storage reservoirs engineered for municipal drinking reserves and industrial cooling reservoirs.
Request Technical Data
Certified high-temperature smoke venting axial fan systems providing rapid air clearance during structural emergency contingencies.
Request Technical Data
Galvanized structural duct fire and smoke dampers engineered with rapid-response thermal shutoff triggers for commercial structures.
Request Technical Data
Underground structural steel-concrete modular water retention chambers maximizing surface site utilization while ensuring water pressure reserves.
Request Technical Data
Continuous-duty industrial ventilation fans dynamically engineered to sustain continuous operation under thermal fire conditions.
Request Technical Data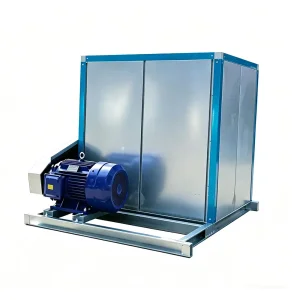
Acoustically insulated double-skin steel fan cabinet designed for low-noise indoor plant rooms, commercial basements, and lab complexes.
Request Technical Data
Combines high volumetric airflow of axial fans with static pressure capacity of centrifugal fans in a compact inline duct configuration.
Request Technical DataAuthoritative technical answers to common queries submitted by procurement teams, mechanical consulting engineers, and plant maintenance directors.
We utilize verified tube pitch, serpentine circuit spacing, surface-area-to-internal-volume ratios, and certified fan performance curves matching original Imeco technical datasheets. This ensures equivalent or superior heat transfer coefficient (U-value) without requiring chiller or pump recalculations.
Yes. We custom-fabricate complete replacement serpentine coil bundles in continuous hot-dip galvanized steel or SUS304/SUS316 stainless steel. We build to existing casing dimensions, flanged connection coordinates, and structural bolt hole centers for seamless installation.
Closed-circuit cooling towers completely seal the process fluid inside clean internal coils. This protects expensive chillers, induction power supplies, and process equipment from airborne particulates, scale formation, oxidation, and biological growths, significantly extending capital asset lifespans.
We supply round carbon steel tubes, elliptical aerodynamic tubes for reduced air pressure drop, and seamless SUS304/316 stainless steel coils. All steel coils are fully welded, pressure tested to 2.5 MPa, and hot-dip galvanized in an automated molten bath.
We integrate high-efficiency cellular drift eliminators certified to restrict droplet loss below 0.001% of circulating volume. Our sloping basin designs prevent stagnant water zones, and optional UV disinfection or automated biocide dosing manifolds are available upon request.
We provide IP55/IP66 class F/H insulated high-efficiency motors, TEFC cast iron explosion-proof designs (ATEX/IECEx certified), direct-drive variable-speed permanent magnet motors, and heavy-duty gearboxes paired with low-noise aluminum or FRP wide-chord airfoil fans.
Please provide: total heat rejection load (kW or MBH), circulating water flow rate (m³/h or GPM), entering water temperature, desired leaving water temperature, local design ambient wet-bulb temperature, power supply voltage/frequency, and site footprint limitations.
Our cooling towers are modularly sectionalized to fit standard 40ft Open Top or High Cube shipping containers without exceeding road transport widths. Casing corners feature heavy-duty lifting trunnions, and structural steel components are secured on custom shipping skids with moisture barriers.
